Posted by PDI on | Comments Off on Complex Molded Parts: When to Integrate and When to Assemble
Today’s complex injection molded parts and assemblies for critical applications are asked to do more than simple one-shot components. They must meet stringent functional demands, operating environment specifications, and often meet aesthetic requirements as well.
For instance, a single housing may need threaded bosses, sealed internal channels, snap features and a clean surface that hides every line. This is rarely achievable with a single, simple tool.
In these situations, design teams are faced with a big question: how do we tackle this? Can it be done as one complex integrated part? Should it be broken into simpler components that can later be joined? Can the whole process be automated, or will it require manual labor? Ultimately, the answer usually depends on the complexity and geometry of the end product. In this post, we’ll look closer at what it takes to produce complex parts. We’ll look specifically at the role of secondaries, strategic assembly, and integrated design.
What Is Integrated Design in Plastic Injection Molding?
Integrated design in injection molding is a method that combines multiple materials, functions, or separate components into a single finished part during the molding process. The most common integrated approaches are:
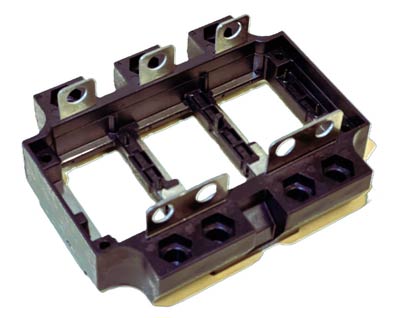
Insert molding – where preformed components are precisely placed inside the mold cavity before the plastic is injected. These typically include metal thread inserts, pins, sensors and other functional parts.
Overmolding – when a second material is molded over or onto a preformed substrate.
Two-Shot Molding – also known as dual-shot or multi-material molding. This molding process relies on two-stage injection. Each stage molds a different plastic within a single machine.
What Are the Benefits of Integrated Design?
There are several advantages to this approach. First, there are fewer parts and lower costs. The process reduces secondary assembly labor, fasteners and manual alignment steps. Further, finished components have higher strength and durability. Especially when compared to gluing, snapping or other joining methods. Better sealing is another benefit, making the components resistant to leaks, vibration issues and dust ingress.
There are some drawbacks as well. The biggest is that tooling typically gets more expensive than simple ones. Creating undercuts and certain internal features may require side actions, lifters, or collapsible cores. These all add to the tooling’s complexity and also complicate maintenance. Though generally speaking, if the part or assembly requires features such as living hinges, integrated snaps, and molded-in threads, integration often wins on overall price. This is especially true for higher volume runs. Material compatibility can also be an issue, particularly for overmolding, and should be considered carefully.
Secondary Operations
Certain complex parts along with their overall job requirements such as run volume may not be practical or profitable to produce with integrated methods. Instead, employing secondary operations might be the better route. For instance, joining certain parts of dissimilar materials or finishes is often easier through secondary operations. Sometimes, parts have internal geometry that can’t be molded as one piece. For these cases, each part can be molded simply, to its required spec and material, then joined afterward. Approaches include:
Ultrasonic Welding – creates strong hermetic bonds along with clean cosmetic results.
Snap Fits – flexible features, such as hooks or cantilever beams, molded into one part. They deflect and lock into a mating feature on another part, allowing for fast, fastener-free assembly.
Post-Mold Inserts – add threads and wear surfaces via ultrasonic or heat-staking instead of complicated tooling.
The Role of Automation
Let’s not assume integrated parts mean fully automated ones. Automation is a separate consideration that can apply to either integrated parts or secondary operations. For example, robots can load inserts for insert molding. Also, automated ultrasonic welding and insert placement can run alongside molding as secondaries. Automation can shift the cost balance of either approach.
Design the Part and Process Together
The biggest mistake we see clients and prospects make is designing parts without thinking much about what it takes to produce them. Both aspects must be considered in the early phases. As for the process itself, the best place to start is with part geometry. If multiple tool actions are required to produce it, then determine if a split eliminates them. Once geometry is out of the way, weigh performance requirements, materials, cosmetics, volume and the likelihood of design changes. Then assess if automation can be a benefit, depending on complexity and run size versus manual labor costs. Make sure to include tooling costs as part of your calculations, not just piece price alone.
Bottom line is to make these calls before tooling is cut. Consider molding and the potential role of secondaries and automation together. Doing so will help ensure a successful program that delivers predictable parts and performance over time.
Posted by PDI on | Comments Off on Insert Molding Best Practices for Critical Applications – Part 2
This is the second installment of a 2-part blog on Insert Molding for Critical Applications. If you missed the first half, you can find it here.
Previously, we discussed this importance of material selection, surface treatment, and chemical compatibility for demanding insert molding components. Today, we will cover the other critical factors including insert placement strategy, thermal considerations, and quality assurance. Let’s dive in!
Insert Placement Strategy
As with other considerations, insert placement is also determined by the demands of the application. (In this context, we’re not talking where the insert will be placed, where talking how.) Generally speaking, consumer applications are more forgiving, and may tolerate ±0.010 inch variation. Conversely, medical devices or aerospace components often require ±0.002 inch or tighter. Volume becomes a factor as well. For low-volume, high-consequence parts, nest fixtures with positive mechanical locators will get the job done. However, high-volume production typically requires vision-guided robotic placement with real-time verification.
Thermal Considerations
Thermal dynamics present yet another challenge to insert molding. The fundamental issue is that you have to manage heat transfer between a metal mass with thermal conductivity 1,000 times greater than plastic and a polymer melt that’s degrading every second above processing temperature.
The secret to resolving this dilemma is setting the right preheat temperature. Insufficient preheat will cause premature freezing and incomplete encapsulation. Conversely, excessive preheat can degrade thermally sensitive resins or cause flash. The target range will change based on the material itself.
Independent control circuits for mold temperature zoning around inserts will go a long way too. To prevent cold spots and flow hesitation, we’ve found it beneficial to heat the area immediately surrounding the insert, making it 20°F-40°F warmer than general cavity temperature.
One final thermal consideration for critical insert molded parts is the cool down phase. Parts left to cool in ambient air tend to develop residual tensile stresses at the plastic-metal interface, leading to cracks. Controlled slow cooling or post-mold annealing can reduce residual stress by a significant amount, dramatically improving long-term reliability.
Quality Assurance
Quality assurance for critical insert-molded components requires more than just your usual go/no-go dimensional checks. If delamination under thermal shock is a challenge, ultrasonic C-scan inspection may be used. When electrical continuity is critical, electrical testing becomes mandatory, even though it drags the production process out.
For the most critical applications, establish protocols that will best simulate end-use conditions. These include accelerated thermal cycling, vibration testing, and destructive pull-out testing. In regulated industries, traceability linking insert lot numbers, resin lots, process parameters, and inspection results to each serialized part enables root cause analysis when failures occur and demonstrates due diligence in qualification and control.
Final Thoughts
As you can see, insert molding for demanding parts requires a lot of additional design and production considerations when compared to conventional components. All deserve equal attention. Getting any one of these wrong will have a significant impact on the insert molded component’s ability to perform its intended function reliability over time. However, now that you know the key considerations, insert molded part success is well within reach.
Have a question about an insert molded part or assembly? Reach out to us, we’re happy to help.
Posted by PDI on | Comments Off on Insert Molding Best Practices for Critical Applications – Part 1
Insert molding is a type of injection molding method that allows a pre-formed metal component to be placed within the molded part. A great example is a battery connector – where the metal is required for conductivity, while plastic offers design flexibility. Designing insert molded parts and processes for more demanding applications is not without its challenges. This is especially true when considering the several variables involved such as material types, positioning of the insert, thermal considerations, and quality assurance. In this two-part blog series, we’ll review each of these considerations, and how to best optimize them for long lasting performance and reliability.
As with all injection molding, both part and mold design are critically important for part success. This is particularly true for mission critical components in demanding applications such as steel blades in medical instruments or reinforcement studs in aerospace components. Since failure can result in safety hazards or premature part failure, engineering becomes more complex than standard injection molding.
Metal Insert Selection
As you can imagine, selecting the right metal for the job is another crucial aspect. Ultimately, the material selection must balance several competing requirements that are specific to the application. While there are many to select from, below are a few of the more popular ones for insert molding:
Thermal Stability – metals must withstand the high temperatures of the injection molding process, which can range from 400-600° or higher. Brass and stainless steel both perform well here, but end-use factors come into play. When considering mechanical loads, environmental threats, and electrical/conductivity requirements, brass and stainless often fall short.
Electrical Requirements – for high current applications, copper alloys are often selected due to their excellent conductivity, despite their higher thermal expansion coefficients.
Weight Considerations – certain applications, particularly those in aerospace and defense, are weight-sensitive. The goal is to have the lightest components possible without sacrificing performance. Aluminum serves weight critical applications quite well, however galvanic compatibility must be carefully considered. This is particularly challenging when dissimilar metals may come into contact within the presence of moisture or certain chemicals. For instance, you wouldn’t want an aluminum insert in a brass housing. This is a recipe for failure, as the aluminum will surely corrode.
Surface Treatment
While surface treatment is often an aesthetic consideration, for insert molded parts, it’s very much a function of performance. Surface treatment must meet the stress demands that the part will be subjected to. If there is particular concern that the insert might loosen or pull out, knurling works well to prevent this. Knurling leaves a textured pattern of ridges grooves, or cross-hatching, giving the part gripping strength. Once the plastic cools around the knurled insert, it creates a “mechanical lock”, which prevents it from slipping out.
Chemical Compatibility
Another key factor for long term insert molded part reliability is making sure that your components are prepared to stand up to the chemicals they will be exposed to throughout their life. This goes beyond the obvious resin-metal interaction during molding. You must consider long-term exposure to operating fluids, cleaning agents, and other environmental contaminants. Then make material selections and insert placement decisions accordingly.
To Be Continued…
Material selection, surface treatment, and chemical compatibility are just three of several key considerations for demanding insert molding components. Check out the second part of this blog where we cover insert placement strategy, thermal considerations, and quality assurance.
Have A Question About a Demanding Insert Molded Part or Assembly?